Contact form
Rip family
Straight rip work for timber and board on SA workshop saws.
Use our contact form when the saw, timber species, and motor size are known. Open Setup guide before fitting a fresh 24T or 30T blade to check projection above the stock and fence alignment. Under Care, keep pitch off the carbide tips and wipe Highveld dust from both flanges before the next rip run.
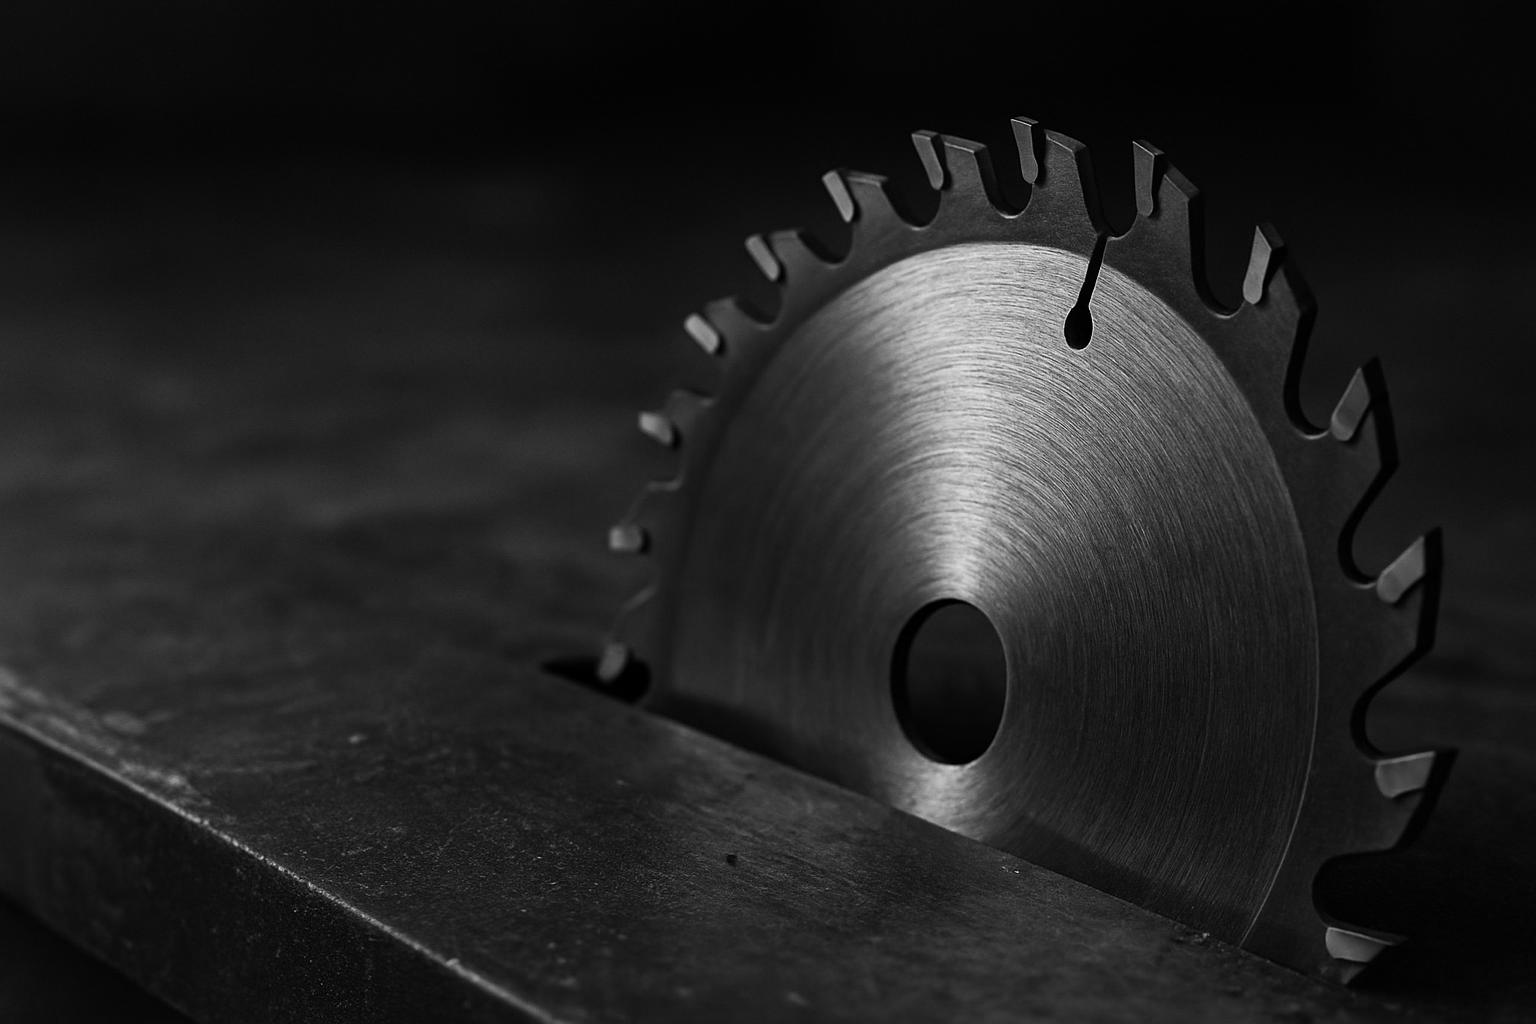
This Carbide Rip Blade is for straight ripping in timber and board where feed speed matters more than a polished crosscut face. With a 3.2 mm kerf and 30 mm bore, it suits the workshop saw setups commonly found in Gauteng joinery and cabinet work. Keep that first board photo with the kerf visible, because it shows drift, burn, and fence error before a full stack is committed.
Choose 24T when thicker solid timber needs waste cleared fast along the grain. Move to 30T where the stock is lighter, the machine is smaller, or the edge needs less tear before planing or further machining. Arbor washers, flange faces, and the riving knife all need a look before spin-up, especially after a dusty shut-down.
Dont skip the first board photo. Every commissioning pack includes a brief card and a tip to photograph the first board with the kerf in frame. That is the difference between a smooth restart and a scrap message at 05:40.
The useful pairing here is not fancy paperwork but the right saw settings for ripping pine, saligna, gum, and sheet products used as straight cut components. Operators usually want tooth count, kerf width, and a quick note on feed pressure in one place. Where stock choice affects cut behaviour more than the blade itself, follow Materials and compare the timber or board note first.
Read the blade note together with Kerfs when the saw starts pinching, heating, or throwing dust instead of chips. If you use our contact form, include the stock thickness, blade diameter, motor size, and whether the trouble shows on entry or exit of the cut. On inland sites, a second flange wipe in the morning is often worth doing before blaming the carbide.
Johannesburg dust loads up saw cabinets, flange seats, and guards faster than many teams expect, especially on dry winter mornings. At the coast, moisture and stored board movement can change how a rip cut opens behind the blade. Daily South African workshop use puts the focus on what affects a Carbide Rip Blade, not showroom talk.
When load-shedding interrupts a run, mark the board, clear the offcut, and check that the blade has not picked up resin before restarting. In Durban or Gqeberha, surface moisture on timber can alter feed feel even when the machine sounds normal. If the saw needs attention beyond blade selection, say so in the email and compare options with Workshop Spares Kit rather than forcing a rip blade to cover a machine fault. Where a scorer is part of the line, set its height separately and do not assume the main blade kerf note answers both.
Operated by Astros Marketing (Pty) Ltd from Sunnyrock 1401, with the shop in Kya Sands, Johannesburg.
| Teeth / grind | 24T / 30T |
|---|---|
| Kerf | 3.2 mm |
| Bore | 30 mm |
| Notes | Highveld dust; keep riving knife honest. |
Keep the core figures close to the machine: 24T or 30T, 3.2 mm kerf, 30 mm bore. Those numbers help the fitter confirm arbor fit, knife compatibility, and expected chip clearance before the first cut. For a bay layout note or saw-side check list, use the contact form and name Carbide Rip Blade clearly.
Use our contact form when you need to discuss ripping stock on a specific saw in Kya Sands, Johannesburg. Include material type, board thickness, blade diameter, and whether you are running 24T or 30T, so we can match the blade to the job.
Verified Google reviews