Contact form
Sheet metal
For light-gauge sheet work, start with the Setup guide before fitting the slitter on the machine bore. Keep the blade clean, oil lightly between runs, and use the Care note after cutting galvanised strip or flashing. If you need sizing or bore details, Send us a message with the material and thickness.
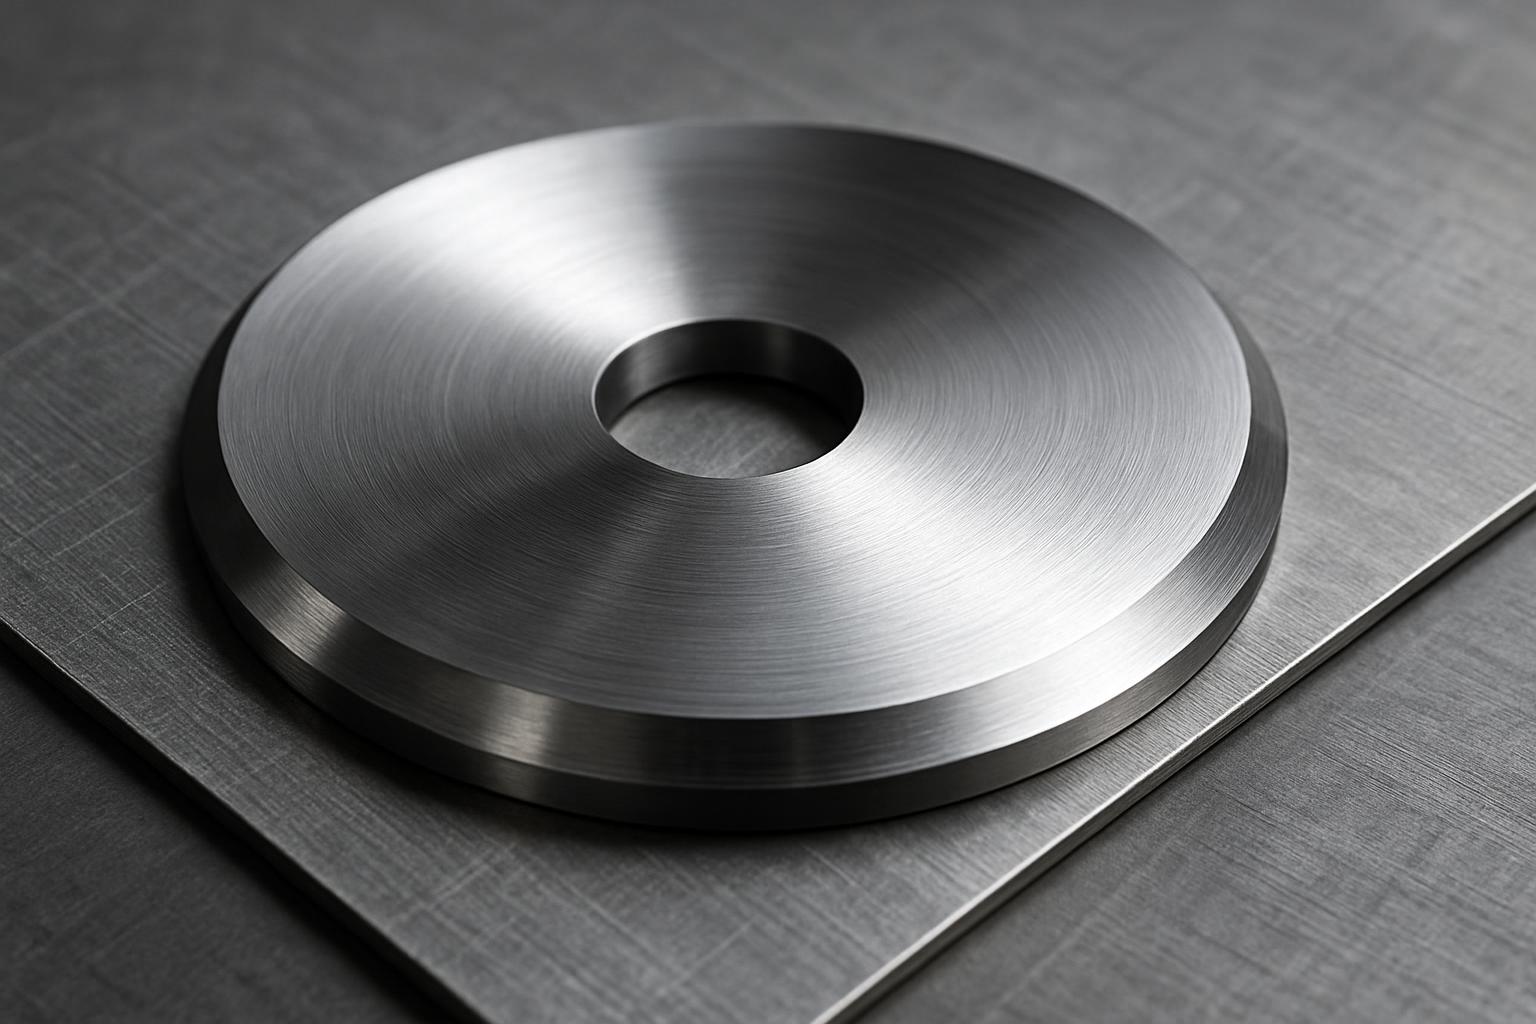
An HSS Slitter is used where neat narrow cuts matter on thin sheet, coil-fed strip, and flashing. In South African fabrication shops, that usually means galvanised sheet, mild steel light gauge, and roof flashing that must stay straight through the cut. The 1.2 mm kerf helps reduce waste while keeping the slit consistent.
Set the blade with square guides and check that the bore seats cleanly on the machine arbor before tightening. Thin material shows every setup error, so side pressure, guide alignment, and feed rate need attention from the first strip. HSS suits this type of work because it handles fine slitting duties cleanly when the material is not overly thick.
Before a full run, cut a short sample and inspect both edges for burring, wander, or heat tint. Flashing stock can mark easily, so a quick first-piece check saves rework on folded or visible sections. Look at the slit line under good light, especially on pre-coated or galvanised material.
Clean slitting of light-gauge sheet with an HSS blade depends on the right blade details, the 1.2 mm kerf reference, and handling notes suited to workshop cutting conditions. For matching stock to blade type, see Materials after confirming the sheet grade and finish.
Read the kerf note with the machine setup, because thin sheet reacts quickly to poor alignment. Use the guidance under Kerfs when you need to compare slit width against the finished part requirement. If you contact us through our contact form, include the metal type, sheet thickness, and arbor or bore size now fitted to the machine.
Highveld dust, coastal moisture, and stop-start power conditions all affect thin-sheet cutting more than many operators expect. A lightly oiled HSS Slitter resists surface rust better when stored properly, but the blade still needs wiping before use. On flashing and coated sheet, cleanliness around the guides matters as much as sharpness.
Near the coast, condensation can leave fine moisture on stored sheet and on the blade body, so inspect both before startup. Inland workshops often battle dust settling on arbors and guide faces overnight, which can push the blade slightly off line. Where machines restart after outages, recheck guide squareness and confirm the strip feeds true before resuming production.
Operated by Astros Marketing (Pty) Ltd from Sunnyrock 1401, with the shop in Kya Sands, Johannesburg.
| Teeth / grind | slitter |
|---|---|
| Kerf | 1.2 mm |
| Bore | machine |
| Notes | Oil lightly; keep guides square. |
The key details for this blade are straightforward: HSS slitter form, 1.2 mm kerf, and bore to suit the machine. Use the setup notes to match the blade to light-gauge sheet rather than heavier plate or bar. For fitment questions or sizing confirmation, use the contact form and send the current machine details.
Send blade queries through our contact form with the sheet material, thickness, and required slit width. Add the machine bore or arbor size so the HSS Slitter can be matched correctly for your setup.
Verified Google reviews